Gauge R&R (also written Gage R&R or GR&R) tells you how much of the variation in an AOI measurement comes from the inspection system itself and from how it is operated, rather than from the boards. Cpk tells you whether the process the AOI is measuring, such as component placement, stays inside its specification limits. Run Gauge R&R first: a Cpk calculated with an incapable gauge describes the gauge, not your process.
What does Gauge R&R mean for an AOI system?
A Gauge R&R study splits measurement variation into two parts. Repeatability is the spread you get when the same board is measured again and again on the same machine by the same operator. It reflects the camera, lighting, clamping and algorithm.
Reproducibility is the spread between appraisers. On a manual gauge the appraiser is a person holding a caliper; on an AOI it is usually the operator loading and clamping the board, or a second machine running the same program.
The result is normally reported as %GRR, the gauge variation as a percentage of either the part tolerance or the total observed variation, plus the number of distinct categories (ndc) the system can resolve.
AOI makes two kinds of output, and each needs its own study:
- Variable measurements, such as X/Y placement offset in µm, rotation in degrees, or component height in µm on a 3D machine. These use a classic variables Gauge R&R.
- Attribute decisions, the pass/fail call on each component. These use an attribute agreement analysis against boards whose condition is already known.
What does Cpk mean when the data comes from AOI?
Cpk compares the spread and centering of a process with its specification limits: Cpk = min(USL − mean, mean − LSL) ÷ (3 × standard deviation). A Cpk of 1.0 means the nearer limit sits exactly three standard deviations from the mean.
As a worked example, take a placement offset specification of ±75 µm, a measured mean of +10 µm and a standard deviation of 15 µm. Cpk = min(65, 85) ÷ 45 = 1.44.
AOI is a convenient source for this data because it already measures every component on every board. Keep the distinction clear, though: placement Cpk describes the placement process. It says nothing about how well the AOI catches a missing part or a solder bridge; that is what the attribute study is for.
What results are good enough?
The thresholds below are common rules of thumb in electronics and automotive supply chains. Your customer's quality agreement always takes priority.
| Metric | Common guideline | How it is usually read |
|---|
| %GRR | Under 10% | Measurement system acceptable |
| %GRR | 10% to 30% | May be acceptable, depending on the characteristic and the cost of improvement |
| %GRR | Over 30% | Not acceptable; fix the measurement before using the data |
| ndc | 5 or more | The system can separate parts into enough distinct groups |
| Cpk | 1.33 or higher | Frequently requested minimum for an established process |
| Cpk | 1.67 or higher | Often requested for new or safety-critical characteristics |
How do you run a Gauge R&R study on an AOI?
The structure is the same as any variables study. What changes on an AOI is what counts as an "appraiser" and what you have to freeze before you start.
| Step | What to do | Typical setup |
|---|
| 1. Define the characteristic | Pick one measurement and its specification limits, for example X offset of a 0402 chip resistor | One characteristic per study, limits in µm |
| 2. Select the boards | Choose production boards that span the normal process range, including some near the limits | 10 boards |
| 3. Select appraisers | Use the operators who normally load the machine, or several machines running the same program | 2 to 3 appraisers |
| 4. Freeze the program | Lock the program version, thresholds and lighting; no program edits or model updates during the study | One program revision, recorded |
| 5. Run randomized, blind trials | Each appraiser loads every board in random order, fully unloading and reloading each time | 2 to 3 trials; 40 to 90 measurements in total |
| 6. Analyze | Use the ANOVA method to calculate repeatability, reproducibility, %GRR and ndc | %GRR against tolerance and total variation |
| 7. Act on the result | If repeatability dominates, look at the machine, fixture or board support; if reproducibility dominates, look at the loading procedure and training | Re-run after any fix |
For the attribute study, build a sample set of good boards and boards with known defects, verified by a reference method such as microscope review or X-ray. Run each sample through the AOI several times and report agreement with the reference, the escape rate and the false call rate.
What should you control during the study?
An AI-based AOI adds one variable a rule-based machine does not have: the model can change. On DaoAI machines, reporting a false call adds an example but does not change the program. The program only changes when someone with that permission runs an AI Update, and that update can be undone.
So for a clean study, record the program revision, agree that no one runs an update until the study is complete, and use locked parameter values for anything the study depends on. Permission levels let you restrict who can program, tune and train, or inspect only.
Also let the machine reach a stable operating state before the first trial, use the same board support and clamping throughout, and keep board warpage within what the machine's clamping and focus can handle.
What does DaoAI's production integration provide?
Gauge R&R and Cpk are part of DaoAI's production integration, which belongs to the same core software on every machine in the range. It includes:
- Gage R&R (GR&R): a repeatability study run in the software on your boards, covering placement X offset, Y offset and rotation angle, and reported as precision-to-tolerance (%P/T) against the AIAG guideline: under 10% good, 10% to 30% marginal, over 30% not acceptable.
- Process capability (Cpk): Cp and Cpk with specification limits, mean, standard deviation and histogram, calculated from the placement measurements the machine already takes, by reference designator or part number, with export to Excel.
- First pass yield: whole-board and sub-panel FPY, with per-position yield in a panel.
- Inspection history and reports: every inspection stored with its images and verdict; reports and all analysis views export to Excel.
- MES export: CSV results, defect crop images and the whole-board image per unit, with defect codes mapped to your MES vendor codes.
The built-in Gauge R&R and Cpk cover placement accuracy only: X offset (mm), Y offset (mm) and rotation angle (degrees). Solder, area, height, coplanarity and OCR results are not included. Because the measurement is fully automated, with no operator-to-operator variable, the study reports repeatability rather than reproducibility, and it does not report %GRR against total variation or ndc. Attribute agreement analysis on pass/fail calls is not built in: you can export each inspection verdict with the operator's review decision and analyze them in a tool such as Minitab.
On the P5 3D inline machine, available for delivery now, component height is also measured rather than inferred, with a reference height accuracy of ≤ 6 µm (≈ 0.236 mil) using the calibration tool. Before a machine ships, a DaoAI engineer will confirm the gauge study, the MES format and the line handling with your team.
How do you keep inspection capability proven over time?
A Gauge R&R is a snapshot. Re-run it after anything that could change the measurement: a camera or lighting service, a machine move, a new fixture, or a significant program revision.
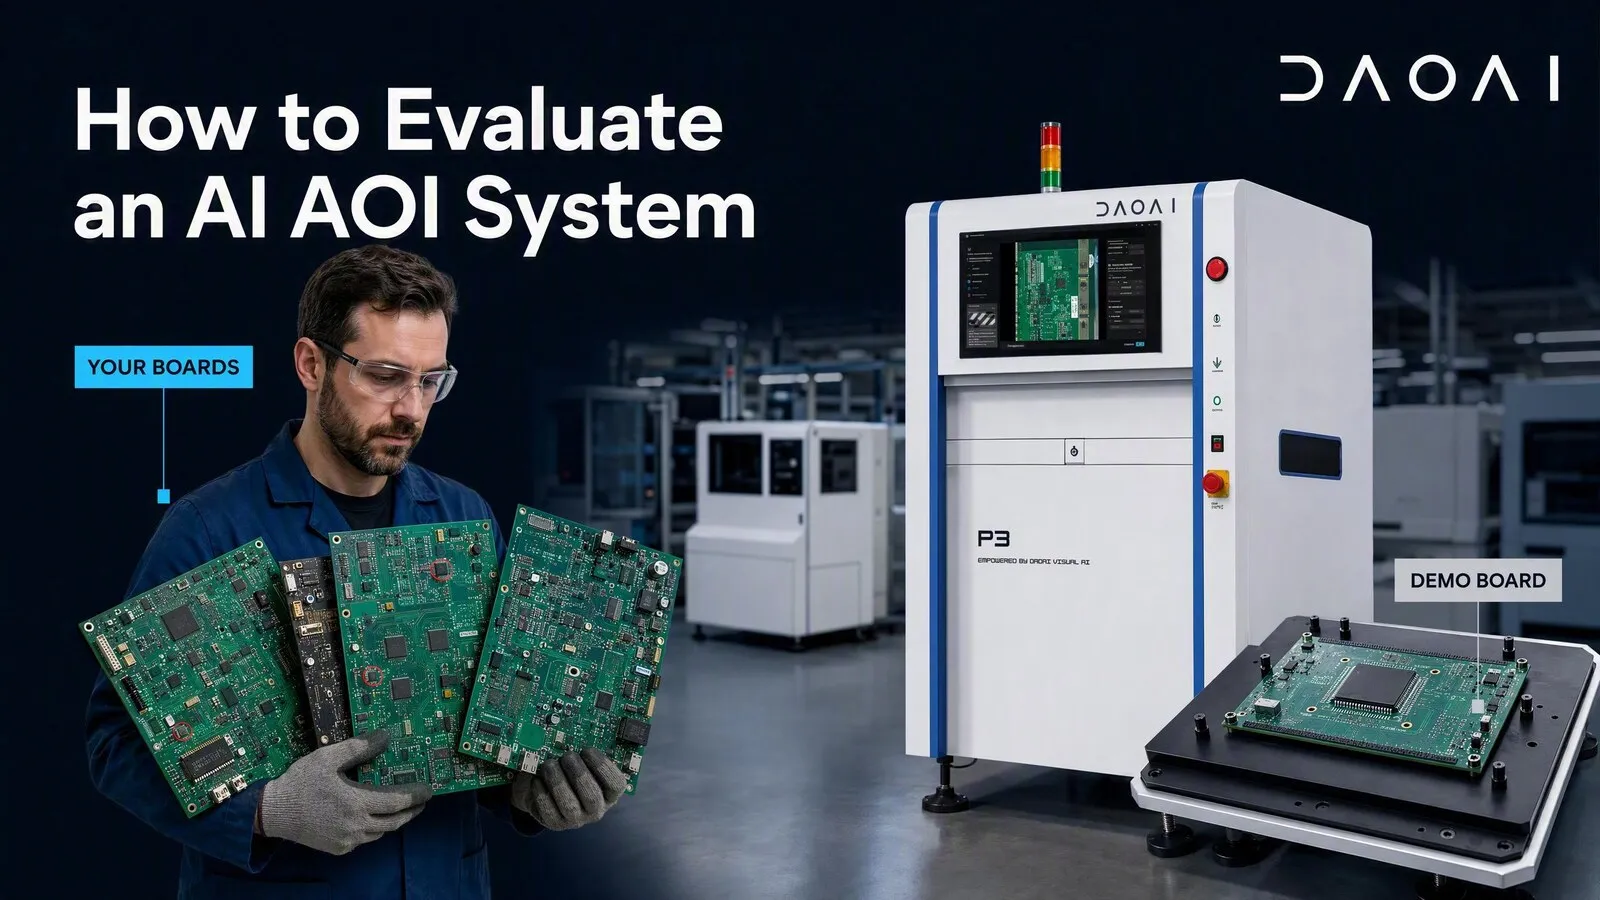
Keep the evidence together for customer audits: program revision, board serial numbers, operators, dates, raw data and the exported result. If you are comparing vendors, ask each one to run the same study on the same boards; our guide on how to evaluate an AI AOI system before you buy covers the rest of that trial.
Finally, watch the attribute side in production. A falling false call rate should not come with a rising escape rate. DaoAI's feedback learning lowers false calls by retraining the model on operator reports rather than by loosening thresholds, which is the approach that keeps real defects outside what the model treats as normal.
FAQ
Is Gauge R&R the same as Gage R&R?
Yes. Both spellings refer to the same repeatability and reproducibility study; "gage" is common in U.S. automotive quality documents.
Should I run Gauge R&R or Cpk first?
Run Gauge R&R first. If the measurement system contributes too much variation, any Cpk calculated from its data is unreliable.
Does placement Cpk prove the AOI catches defects?
No. Placement Cpk describes the placement process. Detection capability is shown by an attribute agreement study on boards with known good and known defective conditions.
Who counts as an appraiser in an AOI Gauge R&R?
Usually the operators who load and clamp the board, since loading is the main human influence on the measurement. Some plants also treat two machines running the same program as appraisers. DaoAI's built-in study is fully automated, so it reports repeatability only.
Can DaoAI run the study on the machine?
Yes, for placement accuracy. DaoAI's software runs a repeatability study on X offset, Y offset and rotation angle, reports it as %P/T, and calculates Cp and Cpk from the same measurements with export to Excel. Attribute agreement analysis on pass/fail calls is not built in.
Bring your quality requirements to a 30-minute session with one of our engineers. Book a demo, or send us one of your own boards and we will test it for you, free of charge.